
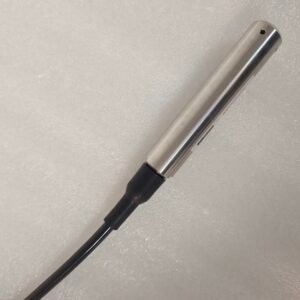
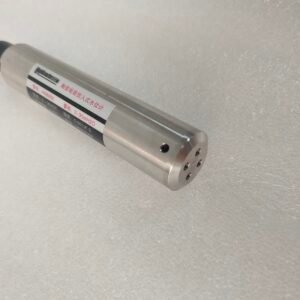
Click here to check more details of the BT8008 ceramic-core level transmitter.
In the industrial production process, liquid level measurement is a crucial link. A liquid level transmitter with excellent performance can not only improve production efficiency but also ensure production safety. In recent years, ceramic core level transmitters have stood out in the market with their unique advantages. Below, let’s reveal the five advantages of the ceramic core level transmitter.
First, accurate measurement, less error
The ceramic core level transmitter adopts a high-precision ceramic pressure sensor with excellent linearity and repeatability. It can keenly perceive the subtle changes in liquid level and accurately convert the liquid level information into an electrical signal output. In the food and beverage production, fine chemicals, and other industries that require high-level accuracy, accurate level measurement ensures that the proportion of the formula is accurate and the reaction process is stable, which in turn protects the consistency of product quality, reduces the rate of defective products, and earns the company a reputation in the market.
Second, corrosion resistance and adaptability
The ceramic core has good corrosion resistance and can resist a variety of acids, alkalis, salts, and other corrosive media. In the chemical, pharmaceutical, and other industries, the production process is often in contact with the liquid has a strong corrosive, ordinary level transmitter is difficult to withstand, and ceramic materials are chemically stable, can resist a variety of strong acid and alkali erosion, to ensure that the level measurement of long-term stable operation, to avoid corrosion caused by measurement errors and even damage to the equipment, greatly extends the service life of the equipment, reduce the cost of enterprise maintenance and equipment replacement frequency.
Third, high temperature performance, wide range of adaptation
The ceramic core level transmitter has good high-temperature performance and can operate in the -40 ℃ to +135 ℃ temperature range of normal operation. In metallurgy, electric power, and other high-temperature operating environments, conventional level transmitters may suffer from high temperatures and performance degradation, but the ceramic core can be maintained at high temperatures to maintain stable physical and chemical properties, support the normal implementation of the level measurement task, protect the continuity of the production process and safety, to help the high-temperature industrial field operate smoothly. This makes it able to meet the needs of different industries for high-temperature level measurement, with a wider range of applications.
Fourth, anti-interference and good stability
The ceramic core level transmitter adopts a fully sealed structure design, effectively preventing external electromagnetic interference. At the same time, the ceramic material itself has high insulating properties, further reducing signal interference. This enables the ceramic core liquid level transmitter to maintain stable measurement performance even in a complex environment.
Fifth, simple structure, easy to install
The ceramic core level transmitter has a simple structure, compact size, and is easy to install and maintain. In the installation process, without complex debugging, it can be quickly put into use. This greatly reduces the user’s installation and use costs.
In short, with its five advantages, the ceramic core level transmitter in the field of liquid level measurement has high cost-effectiveness and wide application prospects. Choose a ceramic core level transmitter to make your production process more intelligent, efficient, and safe.